
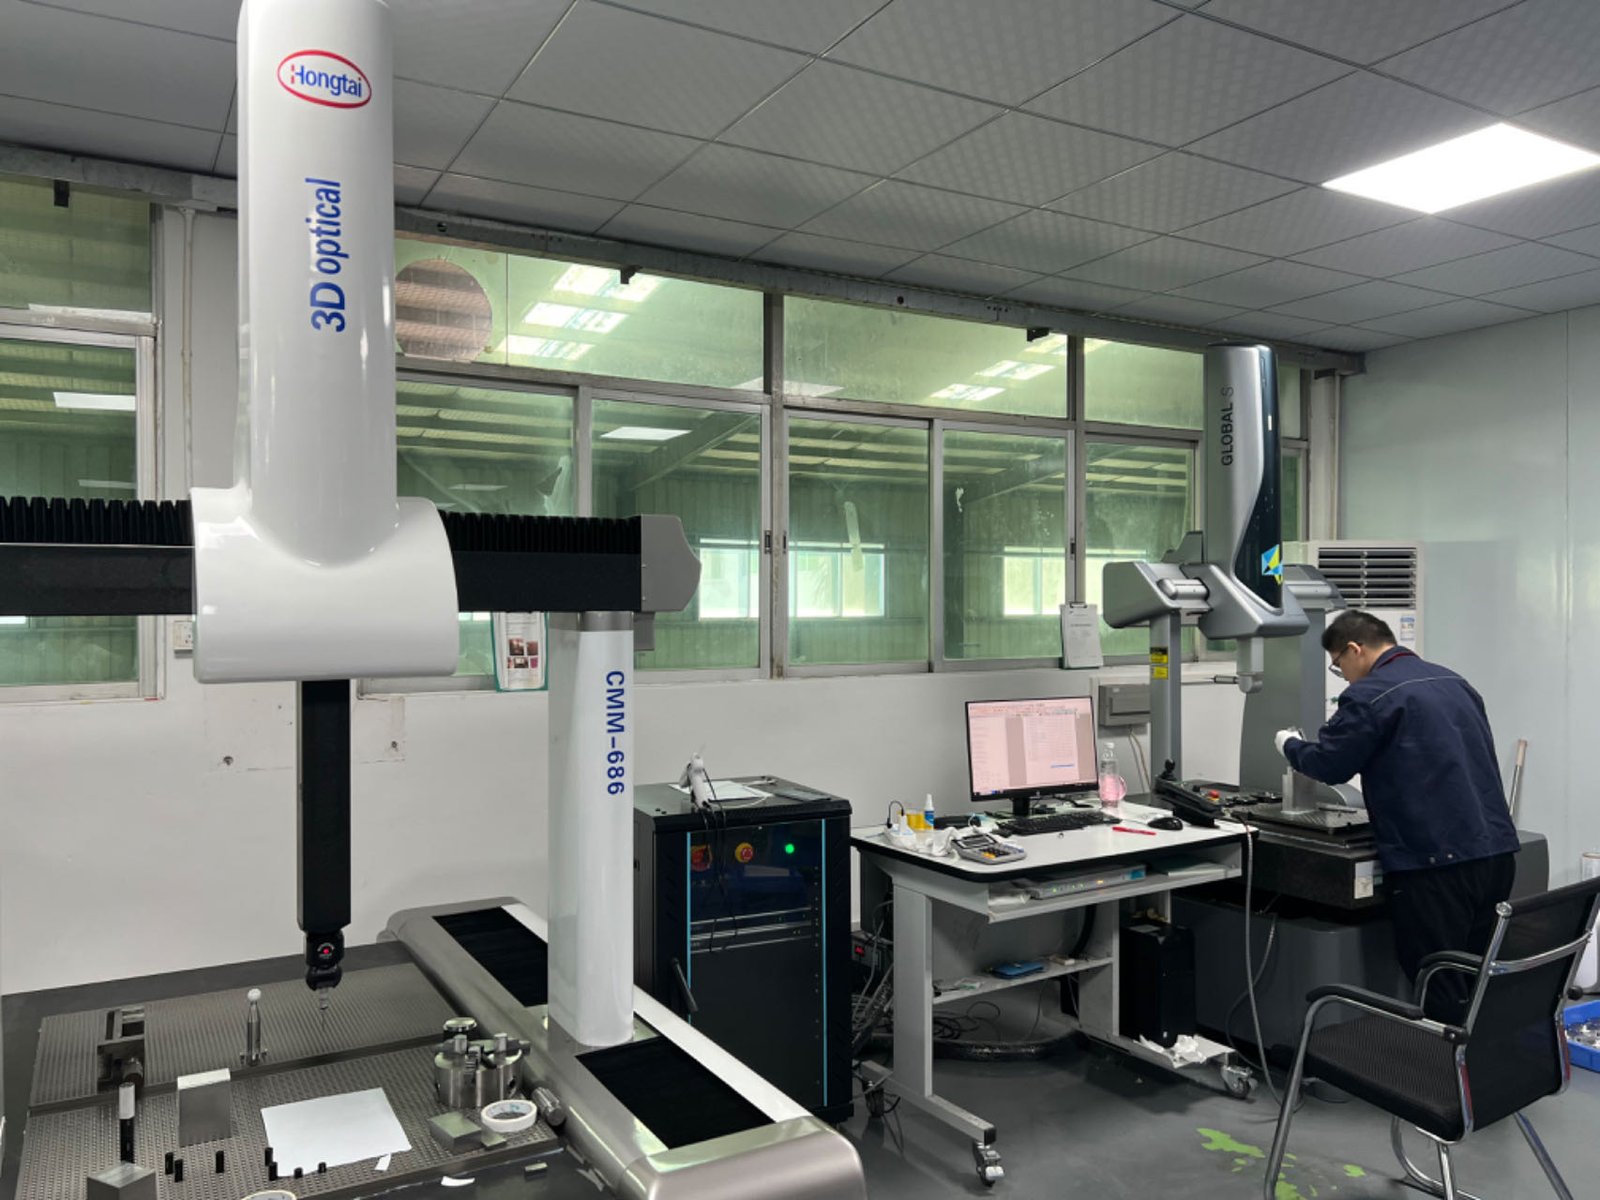
Medical device parts bought from a CNC milling service are judged twice: once on the metal and once on the record. A housing or an instrument component machined to perfect dimensions is not yet a medical part if the material certificate, the finish evidence, and the traceability do not exist, because nobody can tell the difference between a verified part and a lucky one without the documents. This guide walks a buyer through the material choices, the documentation, the tolerance evidence, and the surface-finish and passivation decisions that make a milled medical part verifiable rather than optimistic.
What changes when a milled part is destined for medical use?
A medical part differs from a commercial part in the burden of proof around it. The part may contact tissue, carry a fluid, or sit in the hands of a surgeon, and the consequence of a wrong material or an out-of-tolerance feature is measured in patient harm and regulatory action. That reality flows down to the machining supplier as requirements: the material must be traceable to a certificate naming the exact grade and standard; critical dimensions must carry measured evidence; surface finish must be specified and proven where the part contacts tissue or fluids; and the whole chain must be reconstructable after the fact.
For a component machine shop, medical work is usually build-to-print under the device manufacturer's quality system. The milling service machines to your drawing and holds the material, tolerance, cleanliness, and documentation you specify. ISO 13485 is the quality-management standard for medical devices and typically sits with the device manufacturer or the authorized chain that owns the design; the machining site operates under its own quality system — commonly ISO 9001-based — and works to your requirements. The buyer's job is to flow the requirements down in writing: the material standard, the finish callouts, the document set, and the process records each lot must carry. What is not written into the order does not get produced.
Which materials are typical for medical CNC milled parts?
Medical milling concentrates on a short list of alloys and polymers, and each carries its own verification demands:
| Material | Typical milled parts | What the buyer verifies |
|---|---|---|
| 316L stainless | Instruments, implantable-adjacent hardware, device components | Grade and standard, low-carbon condition, heat/lot number |
| 17-4PH stainless | High-strength instrument and device parts | Condition, heat-treatment record and hardness |
| Ti-6Al-4V ELI | Implantable hardware, long-term devices | Grade, ELI variant, standard, raw-stock certificate |
| PEEK and medical polymers | Device housings, instrument handles, insulators | Medical-grade lot records and material certificates |
| Aluminum 6061-T6 | Non-implant instrument and device components | Temper and standard; finish and anodize record where specified |
Name the material the way the device file names it — the exact grade, the standard (for example an ASTM or ISO reference for implant alloys), and the condition — so the certificate can be checked against the drawing rather than against a family name. On an implantable part, the ELI variant of titanium or the low-carbon 316L is often specified for a reason, and a substitute grade that happens to be close is a material change your quality system must approve before it happens. Put the substitution rule in the RFQ: no change without written approval, and incoming verification of the delivered stock against the certificate before machining.
How is material verified and traced on a medical lot?
Traceability on a milled medical part is a chain of records that starts with the raw stock. Incoming material is logged against its mill certificate, checked by alloy analysis on the lot before cutting, and released with a lot number that ties the stock to the work order, the machine, and the inspection results. When the part is small and unmarked, the lot travels as a unit with its paperwork, which is exactly why lot-based release matters and why a mixed shipment of parts from several heats without segregation is a finding.
The remote check is simple to run. Ask the supplier for a sample traceability record from a past order and follow it yourself: certificate number, incoming verification, dimensional report, and the conformity statement that tied them to the shipment. If the supplier assembles that chain in minutes, the system is real; if the request stalls, no documentation promise for your own order will survive an audit. Learn to read the certificate, not just confirm its presence: the grade must match the standard your device file names, the condition must match, and the heat number must appear on the incoming record. The quality page shows how one milling service structures its material verification, measurement, and reporting — a concrete benchmark for the evidence you request.
What tolerance and finish evidence should a medical lot carry?
Medical parts are not held to a different tolerance than other precision work — they are held to a better-evidenced one. Milling holds fit and alignment features to ±0.003 mm, with process capability at Cpk 1.67 or higher demonstrated on key characteristics; precision grinding reaches ±0.002 mm where seating or bearing surfaces require it. What medical adds is the expectation that critical dimensions are measured and reported as values against the callouts, with the instrument and date identified, because the report is what your quality system signs off.
Surface finish carries more weight on medical parts than on commercial ones. A machined surface that contacts tissue, carries a fluid, or sits in a cleaning and sterilization loop has to be smooth enough not to harbor contamination, and the roughness values are functional callouts, not cosmetics. Specify the Ra value by feature group on the drawing — the faces that contact tissue or fluids deserve a real number and the inspection to prove it — and state whether the value applies before or after any treatment step. The tolerance evidence and the finish evidence together are the two records an auditor reconstructs a device lot from months later.
Why do passivation and treatment records matter on stainless parts?
Machining stainless leaves embedded iron from the cutting tools on the surface, and that free iron is where corrosion starts — on an implantable or surgical part, corrosion is a functional failure, not a cosmetic one. Passivation removes the embedded iron and restores the stainless's natural corrosion resistance, which is why a passivation step and its record belong on the drawing for machined stainless parts. On an anodized aluminum part, the class and coating thickness on the certificate is what the print calls out; on a passivated stainless part, the process record confirms the surface was restored after machining.
Ask which treatments the milling service runs in-house and which route through qualified partners, because the answer defines where the record can break. A passivation certificate from an unverified source is as serious as a missing material certificate on a medical part. Confirm the treatment is part of the quoted scope — adding it after the quote moves both the price and the date — and require the treatment record to travel with the lot, naming the process, the date, and the acceptance criteria. The services overview explains how machining and finishing combine into one order, which is the frame the treatment question belongs in.
Cleanliness and handling sit beside the treatment in the same conversation. A medical part is not finished the moment the last chip is cut: it has to leave the machine free of coolant residue, swarf, and loose burrs, and it has to be handled and packed so it arrives clean. Ask what the service does between machining and shipping — whether parts are cleaned, deburred, and inspected for edge condition, and how they are packed so a finished surface is not damaged in transit. These are not cosmetic questions on a device part: a burr on a sealing edge or a scratched surface on an implantable component is a non-conformance that your incoming inspection must catch, and catching it on the floor is cheaper than catching it at your dock. The cleanliness and packaging expectations belong in the order, alongside the tolerances and the documents.
What documentation should a medical machining lot ship with?
Agree the document set in the RFQ, because on a medical part the records are part of the product. For a qualified lot, plan for:
- Material certificate naming the grade, standard, condition, and heat or lot number of the raw stock.
- Incoming verification record showing the lot was checked against the certificate before cutting.
- Dimensional report with measured values on critical dimensions against the drawing callouts.
- Finish and treatment records for the Ra callouts and any passivation or anodize step.
- Certificate of conformity tying the material, dimensional, and process records to the purchase order and lot.
Name each document in the RFQ and confirm the format matches what your quality system expects, because a lot whose records cannot be mapped to its parts is a lot your incoming inspection cannot release. When the material changes heat or lot between production batches, the record must change with it — a reused certificate on a new lot is a traceability failure that surfaces in an audit even when the parts are perfect.
How do you qualify a CNC milling service for medical work?
Qualification runs in stages, each producing evidence you can audit from your desk. First, confirm the quality-system scope and ask the service to state its certifications plainly — ISO 9001-based systems are the common base for component machining, and the medical-layer requirements flow down in your order. ISO 13485 is the medical-device quality-management standard that the device manufacturer or its authorized chain typically holds; confirm where the requirement sits in your contract rather than assuming the machine shop must hold it. Second, verify material control with the sample traceability exercise above. Third, verify measurement and finish: ask how critical dimensions and Ra callouts would be measured and reported, and in what format.
Then run the qualification itself — a first article machined with the full document set, shipped by courier, and measured on your own equipment against your drawing. Measure the critical dimensions and the surface finish on the called-out features, and match the certificate numbers to the lot. If the first article matches its paperwork, the service's system is real and volume is a scaling decision; if it drifts, the lesson costs one part and one courier shipment rather than a rejected production lot. The parts guide shows the range of milled components that pass through the review before release.
Use the qualification stage to test the record against your quality system's actual format, not just its content. If your incoming inspection expects the dimensional report keyed to your part numbers, ask for the first article's report in that format; if your device file requires a specific material certificate layout, ask for a sample before volume. A service that adapts its reports to your system is a service whose production lots will clear your receiving inspection quickly; one that issues its own format and expects you to translate is deferring the work to every future lot. The format test is cheap on a first article and expensive to discover at the first production shipment, so it belongs in the qualification rather than after it.
How do you keep the chain intact from first article to production?
The chain that the first article establishes has to survive volume, and the protection is written into the order. Repeat the document set in the production RFQ, name the treatments and their record requirements, and state the traceability expectation in the purchase order: each lot released against its own material record, with certificate numbers on the packing list. When the raw stock changes heat between lots, expect a new incoming verification for the new heat, not a reused certificate.
On the first production lot, inspect what the chain claims. Measure a sample of critical dimensions and finish values on your own equipment and compare them to the reports. Check that the certificate numbers on the documentation match the lots you received. Confirm the treatment records name the process the drawing specifies. A lot whose paperwork does not match its parts is a lot to hold, and the documents make the hold defensible. A production lot that matches its paperwork on the first delivery is the strongest evidence that the service's system is real. The factory page shows the floor and equipment behind the machining, and the contact page is where a specific medical drawing becomes a specific qualification conversation, with the material, finish, and documentation requirements named up front.
Frequently Asked Questions
Can a general CNC milling service machine medical parts?
Yes, as a build-to-print component supplier. A milling service machines to your drawing under its quality system and holds the material, tolerance, cleanliness, and documentation you specify. ISO 13485 is the quality-management standard for medical devices and typically lives with the device manufacturer or its authorized chain; confirm the quality requirement your contract imposes on the machining site.
Which materials are typical for medical CNC milled parts?
Stainless grades such as 316L and 17-4PH for instruments and implants, titanium Ti-6Al-4V ELI for implantable hardware, and engineering polymers such as PEEK and medical-grade plastics for device components. Specify the exact grade, standard, and condition so the material certificate can be checked against the drawing.
What tolerance can medical CNC milled parts hold?
Milling holds fit and alignment features to ±0.003 mm, with capability at Cpk 1.67 or higher on key characteristics and Cpk ≥ 1.33 on general characteristics. Capability is reported per characteristic: every report names the feature, its tolerance band, the sample size, the sigma method, and the study window.; precision grinding reaches ±0.002 mm for seating and bearing surfaces. Critical features are measured and reported, not assumed — the record is part of the product on a medical part.
How is material verified on a medical machining lot?
Incoming stock is held against its mill certificate and verified by alloy analysis on the lot before cutting. The certificate names grade, standard, condition, and heat or lot number, and a lot number ties it to the parts and the dimensional report. Ask for a sample traceability record from a past order.
What documentation should a medical machining lot ship with?
The material certificate, the incoming verification record, a dimensional report with measured values on critical callouts, process records for any treatment, and a certificate of conformity tying the set to the purchase order. For validated programs, add the first-article record and the evidence your quality system requires.
Why do surface finish and passivation matter on medical parts?
Because machined surfaces contact tissue, fluids, or the user. A clean surface with controlled roughness reduces crevices where contamination and corrosion start, and passivation restores the corrosion resistance of machined stainless by removing embedded iron. Specify the Ra values and the treatment on the drawing so the record proves them.
How do you qualify a CNC milling service for medical work?
Run a first article with the full document set, shipped by courier, and measure the critical dimensions and finish on your own equipment. Match the certificate numbers to the lot and confirm the report format matches your quality system's requirements. The first article proves the record before volume.
Have a medical drawing that needs a documentation review?
Send the model with the material standard and your documentation list to [email protected] or call +86 13126536955, and the review will come back with the material, finish, and documentation plan in writing.