
How Much Do CNC Milling Services Cost in 2026? A Buyer's Cost Model
On a milled part, the tolerance block is the price list. A drawing that reads "±0.1 mm" on every dimension tells the shop one story; a drawing that anchors its features to datums with true position and profile callouts tells another, and the two can differ in price by more than the machining alone would suggest. The difference is not the tolerance numbers alone — it is whether the callouts can be verified. Geometric dimensioning and tolerancing exists to make a requirement measurable, and measurability is where the cost of CNC milling services actually lives. This guide is the buyer's cost model for CNC milling services in 2026: what a milling quote really contains, why the way you call out a tolerance decides the price before the first cut, how geometry, material, quantity, and verification move each line, and how to write a drawing that gets quoted the way it is meant to be made.
What does a CNC milling services quote actually pay for?
Strip any serious milling quote back to its bones and the same lines appear underneath the formatting, with one addition that matters more than most buyers expect: the verification line, where the tolerance callouts on the drawing become CMM routines and reports.
| Line item | What it pays for | What moves it |
|---|---|---|
| Material | The bar, plate, or block at the grade on the drawing | Grade, form, and whether the lot is verified against a mill certificate |
| Setup and datum strategy | Fixturing each setup from the datum structure, first-piece prove-out | Every datum transfer adds a setup and a chance for error to accumulate |
| Machining time | Spindle minutes to cut each feature into its tolerance zone | Material toughness, feature count, and how tight each band is |
| Grinding | The features a mill cannot hold to their band | A separate process family for the tightest tolerances and hardened parts |
| Verification | CMM time to prove true position, profile, and datum features | Each GD&T callout becomes a measurement routine and a report |
| Finishing and secondary operations | Coating, threading, and similar final steps | Each step adds a line and a sequence; coatings grow the surface |
| Inspection and documentation | CMM reports, SPC records, material certificates, PPAP where required | The evidence trail is part of the product on GD&T work |
There is no honest single number for CNC milling services, because the tolerance block, the material, the quantity, and the verification the drawing demands decide it together. What stays consistent is the structure, and the structure is what makes the price readable and the callouts auditable.
Why does the tolerance block decide the price before the first cut?
GD&T exists because a plus-minus dimension cannot describe where a feature really sits. A hole located by a coordinate is checked to two numbers in two directions; a hole located by true position is checked against the datum system as a relationship, which is what actually matters when the part meets another part. The site behind this guide is built around that distinction — its pages are organized around reading GD&T correctly, not just hitting numbers blindly — and the price follows the same logic.
The tolerance block decides the price in two ways. First, it decides the process: a ±0.1 mm dimension is routine milling, a ±0.003 mm feature is controlled milling, and a feature that needs a tighter band or a fine finish moves to grinding. Second, it decides the verification: a plus-minus dimension may be checked with hand tools, while a true position or profile callout becomes a CMM routine measured against the datums, and every callout the CMM has to prove is a line on the quote. A drawing that calls out GD&T where the function needs it is spending its verification budget where it protects the assembly; a drawing that scatters callouts is spending it everywhere. The way you write the tolerance block is the way the shop has to build and measure the part, and the price follows.
How do datums anchor the price?
A geometric control without a datum is a control that cannot be verified, and a control that cannot be verified has to be priced as risk. The datum scheme tells the shop which features are the reference points everything else is measured from, and it sets the machining strategy: every setup has to locate the part from the datum structure, so a datum chosen well — a feature machined early, stable, and easy to fixture — keeps the setups simple, while a datum that forces awkward re-fixturing multiplies the measurement chain.
The rule for the drawing is short: choose datums that the shop can actually build from, machine the datum features early, and let the functional relationships flow from them. A part whose datums are decided by how it sits in the assembly is a part that measures cleanly; a part whose datums are chosen by convenience is a part whose price carries the cost of the shop guessing at your intent. When a drawing arrives with a clean datum structure, the quote is lower, the setups are fewer, and the CMM program is shorter — all because the reference points were settled before the first setup, not discovered during it.
Which tolerance callouts cost the most on a milled part?
Not all GD&T costs the same, and knowing which callouts carry the heaviest verification load keeps a milling budget honest. True position on a hole pattern is the classic value-for-money callout: it verifies the relationship that governs whether parts assemble, and on a milling floor it is measured on a CMM against the datums. Profile tolerances control a surface's form and location together, which makes them powerful on contoured faces, and more demanding to verify, because the CMM has to sample the whole surface rather than a single point. Form controls such as flatness and straightness verify a surface against itself and are comparatively direct to measure.
The index of this site lists the fourteen GD&T symbols and which ones show up on machined parts; the cost lesson is that each symbol is a different measurement routine. A part that stacks position, profile, and perpendicularity on the same feature pays for each control at the CMM. And the material-condition modifiers change what the shop must hold: a position tolerance at MMC (maximum material condition) grants bonus tolerance as the feature departs from its maximum material size, which is why an MMC callout costs less to hold than the same position at RFS — the process gets room to breathe. Specify the callout the function needs and the modifier the assembly allows, and the verification budget goes where it protects the design.
How much do tolerance and finish move the price on milled work?
Tolerance is the steepest part of the milling cost curve, and it moves in steps rather than a line. A mill holds ±0.003 mm on critical features routinely, and a call at that band on a milled feature carries a healthy process capability. Push the same feature toward ±0.002 mm and the mill is stretched across the band — the process must change, and the feature moves to precision grinding, where surface, centerless, or cylindrical machines hold the tolerance with their own measurement. On this floor, milling and turning hold ±0.003 mm and grinding reaches ±0.002 mm, verified on Hexagon CMMs with process capability at Ppk ≥ 1.67 at the initial study on key characteristics and ≥ 1.33 on general ones, and demonstrated at Cpk = 1.851 on a representative length characteristic.
Read the tolerance band before you read the index. Cpk is a ratio of the tolerance band to the process spread, not an absolute measure of accuracy. The figure above was recorded on a length characteristic with a 0.4 mm band (76.1–76.5 mm) — wide by design. Hold the same process spread against a ±0.005 mm feature and it fails outright. Ask for the band, the subgroup count and the sampling window on every capability number a supplier quotes.
Finish stacks onto tolerance on the same features. A fine Ra on a sealing or bearing face often pairs with a tight tolerance on the same surface, and that pairing is what pulls the feature toward grinding. Specify the finish on the features that earn it, keep the rest on the general block, and read the pairing of tolerance and finish together when you review the drawing — the two callouts belong in the same budget decision.
Which material should a milling budget assume?
Material moves a milling quote twice: once as stock, and again at the cutting edge where the tolerance is being held. Aluminum 6061 is the economical default for milled housings and brackets — it machines cleanly and holds a good finish. The demanding grades — 7075-T6 for higher strength, the stainless grades that work-harden, and titanium — cut slower, wear tools, and make a tight tolerance harder to hold, which pushes the price on every feature that touches them. The materials list on this site's parts page names the range the floor actually runs, and the rule for the budget is the same as everywhere in precision work: name the grade, not the family, because a substituted alloy passes every dimension and fails in service.
Two rules keep the material line honest. First, verify the shop checks incoming stock against its mill certificate — incoming lots on this floor are XRF-checked before they reach a machine. Second, read the material as part of the tolerance problem: a grade that is difficult to machine makes every tight feature on the drawing more expensive to hold, not just the ones that look demanding.
How does quantity bend the unit price on milling services?
The setup on a milled job is the same whether you order one part or a thousand: the fixture, the program, and the first-piece prove-out cost the same either way. At one piece, that fixed cost lands entirely on the part, which is why a prototype looks expensive. As quantity rises, the setup spreads across the run and the unit price falls toward the sum of the material and the machining time.
On GD&T work, the first article carries an extra load, because it proves the measurement as well as the machining: the datum strategy, the CMM routine, and the capability are all established on the first part before the run begins. Use the MOQ of 1 piece the way this site teaches — validate the geometry and the measurement on a single part before committing volume, because the cost of measuring one part is trivial next to the cost of a wrong lot. And budget the reorder at the proven rate: once the fixture, the program, and the CMM routine are documented, the same part ships faster and cheaper, because the setup is no longer a gamble.
What hidden costs sit inside a milling services quote?
The visible lines are half the price; the other half hides in what the quote does not say. A quote that prices sizes but not the GD&T callouts has hidden the CMM routines the drawing actually demands. A quote that absorbs inspection into the margin has hidden the reports you will recreate at incoming. A quote that names a tolerance band but no datum strategy has hidden the setups the part will need. A quote that treats grinding as an afterthought has hidden the process family that owns your tightest features. And a quote from a service that cannot show its CMM bench, its machine list, or its certificate numbers has hidden the verification that is the product.
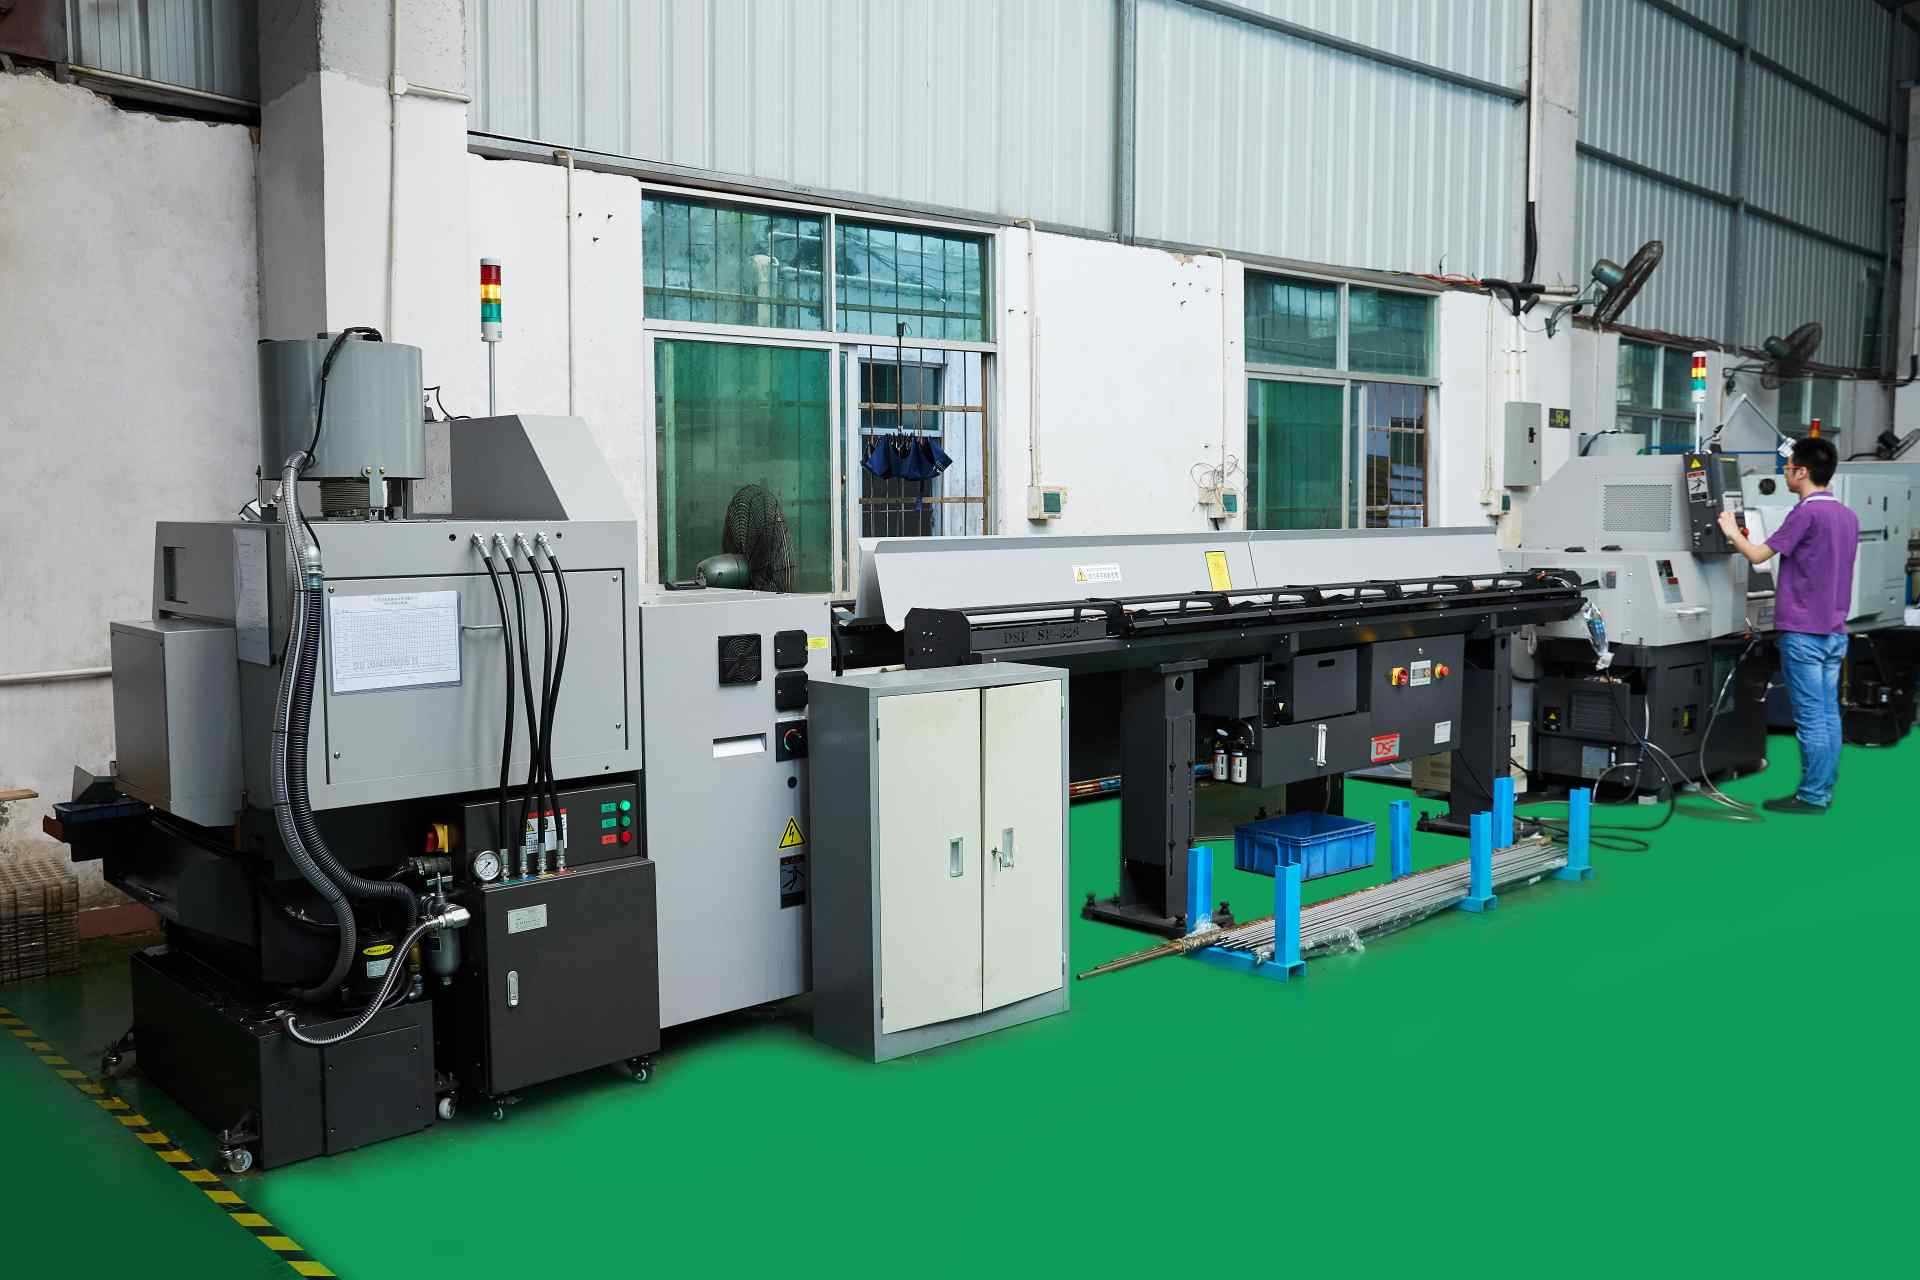
The supplier itself is the largest hidden cost of all. A trading desk adds a margin and removes accountability, and on GD&T work the accountability is the measurement. The brand behind this site is Dongguan Zhuohang Ltd, incorporated in 2005, registration number 91441900MA4UWT6X39, operating a 6,800 m² facility in Hengli Town, Dongguan, with 100+ staff and 100+ production machines — 3-axis (50+), 4-axis (20+), 5-axis (20+), 25+ lathes, and 7+ grinders — plus 20+ inspection instruments, with Hexagon CMMs verifying true position, profile, and datum features. Its certificates carry numbers a buyer can verify: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (product design excluded) (131941/A/0001/SM/En), and ISO 14001:2015 (116024/B/0001/UK/En). When the entity, the floor, and the measurement are checkable in writing, the margin stays in the quote where you can read it.
How do you compare two milling service quotes on the same basis?
A quote you can compare states its assumptions, and on GD&T work the most important assumption is the measurement plan. Make sure every service shows the tolerance and finish it will actually hold per feature, the datum strategy and the number of setups, the CMM routines for true position, profile, and form callouts, the material grade and how the lot is verified, the process families included — milling, turning, mill-turn, grinding — and the quantity tier with prototype and production separated.
Compare the itemized routes at the quantity you actually plan to order, because the same drawing at fifty pieces and at five thousand is two different cost problems — the setup is the same, but its weight per piece is not. And weigh the price against the measurement evidence in the same breath. The lowest quote on milling work is rarely the lowest total cost: the parts that arrive without their CMM reports or control charts are the parts you will pay to measure, sort, or replace. The evidence is part of the product, and a service that treats it as an extra is telling you where its real margin lives.
How do you build a 2026 milling-services budget that holds?
Build the budget the way this site reads a drawing — callouts first, process second, quantity third.
- Write the tolerance block before you ask for a number. Anchor the features to datums, use true position and profile where the assembly needs them, use MMC where the function allows it, and leave the rest on the general block. A drawing that specifies its requirements correctly is a drawing the shop can quote the way it is meant to be made.
- Get the DFM review on the callouts that cost. Send the drawing and ask which tolerances are tighter than the function needs, which callouts are pulling features into grinding, and which finishes add a process step. Fix the drawing first; then budget the fixed part.
- Quote the prototype and the production tier on the same page, and verify before you commit volume. The prototype at MOQ 1 proves the machining and the measurement at full setup weight; the production tier shows where the fixed lines amortize. Budget both at your real quantity, and the 2026 number will survive the first CMM report.
Keep the closing rule in front of you: read the quote as a set of verifiable requirements, not a total, and the milling-services budget you build will hold across the drawing changes, quantity shifts, and reorders that real sourcing always brings.
Frequently Asked Questions
How much do CNC milling services cost in 2026?
No honest service quotes milled parts without a drawing, because the price is set by the tolerance block, the datum strategy, the material, the quantity, and the verification the callouts demand. A simple part on general tolerances at production quantity sits low; a part with true position, profile, and datum callouts at prototype quantity sits far higher. Budget the requirements the drawing actually carries.
Why does GD&T cost more than plus-minus tolerances?
Because GD&T is a measurement requirement, not just a size. A plus-minus dimension may be checked with hand tools; a true position or profile callout becomes a CMM routine measured against the datums, and every callout the CMM has to prove is a line on the quote. The cost buys a relationship that is actually verified.
What tolerances can milling services hold?
Milling and turning hold ±0.003 mm on critical features, and precision grinding reaches ±0.002 mm, verified on Hexagon CMMs with process capability at Ppk ≥ 1.67 at the initial study on key characteristics and ≥ 1.33 on general ones, demonstrated at Cpk = 1.851 on a representative length characteristic.
How do I know the tolerance callouts on my drawing will be verified, not just claimed?
Ask which CMM routine measures each callout, which datum it references, and what the report will contain. True position, profile, and perpendicularity on this floor are verified on Hexagon CMMs — the report is the part of the tolerance you can audit after the parts ship.
What is the minimum order, and do reorders cost less?
The MOQ is 1 piece, so a first article can be machined, measured, and approved before volume is committed. Once the fixture, the program, and the CMM routine are documented, reorders skip the prove-out and ship faster at a lower per-piece rate.
Which company and certificates back the quote?
The brand behind this site is Dongguan Zhuohang Ltd (registration 91441900MA4UWT6X39), incorporated in 2005, at a 6,800 m² facility in Hengli Town, Dongguan, with 100+ staff and 100+ machines, certified to ISO 9001:2015, IATF 16949:2016 (product design excluded), and ISO 14001:2015 with verifiable certificate numbers.
Want a milling quote that matches your tolerance block?
Email the toleranced 2D drawing with the GD&T callouts and a STEP or IGES 3D file to [email protected] or call +86 13126536955. You will get a review of the tolerance block, the measurement plan, and an itemized quote with the prototype and production tiers on the same page.